High Energy X-ray and CT
When a part is too dense for an X-ray tube, a linear accelerator is the only way in. MQS builds turnkey high-energy inspection systems for rocket motors, solid propellants, heavy castings and pressure vessels — installed, shielded and supported in India.
Density Is the Limit. Energy Is the Answer.
A 450 kV tube stops at roughly 80 mm of steel. Beyond that the beam is absorbed before it reaches the detector and the image goes dark — not because the defect is invisible, but because nothing got through.
Linear accelerators produce photons energetic enough to pass through half a metre of steel, or two and a half metres of solid propellant. For more than a decade MQS has delivered off-the-shelf and fully customised turnkey systems built on this principle, for some of the country's most demanding aerospace, defence, energy and heavy-engineering programmes.
Varex Linear Accelerators
Linatron models from 0.95 to 15 MeV, single and dual energy, selected against the thickness and density you actually inspect.
Detectors & Software
Digital flat panel detectors rated to 16 MeV with optional line detectors, driven by MQS Imaging Suite and VG Studio Max.
Manipulators & Enclosures
Multi-axial manipulators for the accelerator head, detector and object, plus shielded enclosures and remote control stations.
What sets the platform apart.
CT-Ready Framework
Upgradeable for 3D computed tomography, extending usefulness and future-proofing the investment.
Dual Energy Linatron
Deep penetration through high-density steel and propellant, with energy selection for different tasks.
Custom Multi-Axis Manipulator
Adapts to complex shapes and orientations — less repositioning, better coverage.
Digital Flat Panel Detector
High-resolution images at fast frame rates for real-time flaw detection with excellent clarity.
Real-Time ADR Software
Instantly identifies cracks, voids and porosity — faster inspection, less operator subjectivity.
Choose by What You Need to See Through.
Every model is defined by one number that matters more than the rest: how much steel it can penetrate. Bars show each model's usable window against a 500 mm scale.
Thickness figures are nominal. Solid propellants can be inspected up to 2500 mm thickness.
Four Ways to Build a High Energy Cell.
The accelerator is one component. What changes between installations is how the beam, the detector and the part are moved relative to each other.
K15 Dual Energy LINAC System
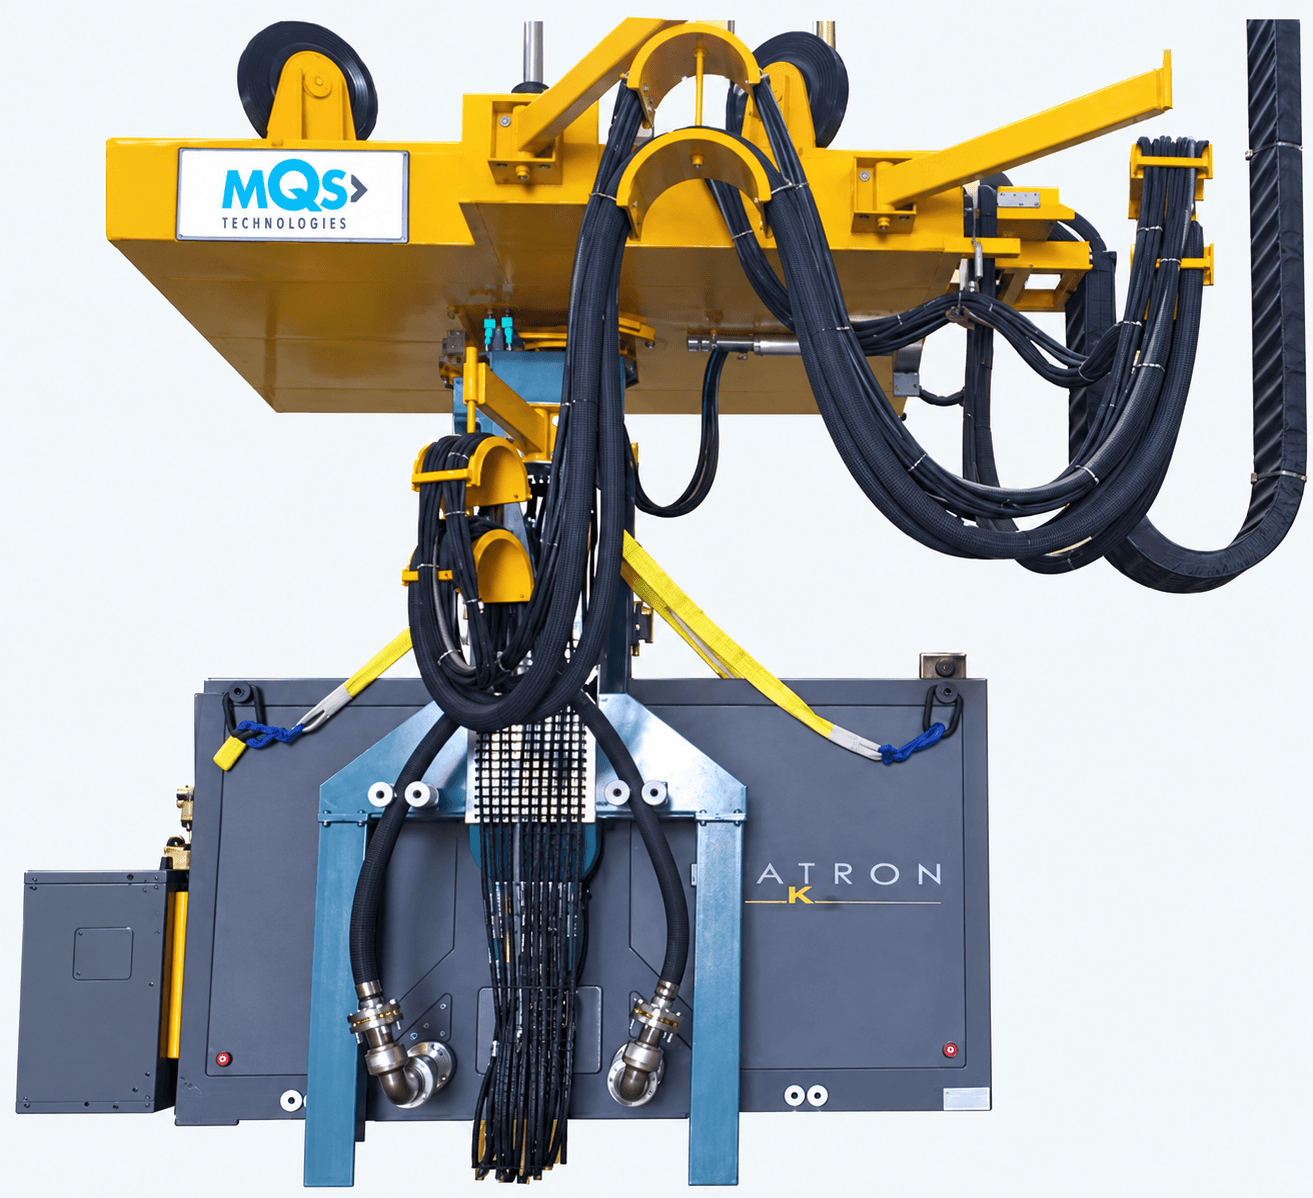
Built around the K15 dual energy accelerator for rocket motors, solid propellants, castings and heavy engineering products — detecting cracks, porosity, inhomogeneities, inclusions and foreign bodies. An EOT crane-mounted head manipulator carries the accelerator, so large objects can be inspected from multiple angles without being repositioned.
- Energy9 / 15 MeV
- Penetration in steelUp to 500 mm at 15 MeV · up to 380 mm at 9 MeV
- Focal spotLess than 2 mm
- Dose rate15 MeV: 40–120 Gy/min-m · 9 MeV: 12–40 Gy/min-m
- Beam symmetryWithin ±5%
- Solid propellantUp to 2500 mm thickness
Digital Radiography with Linear Accelerators
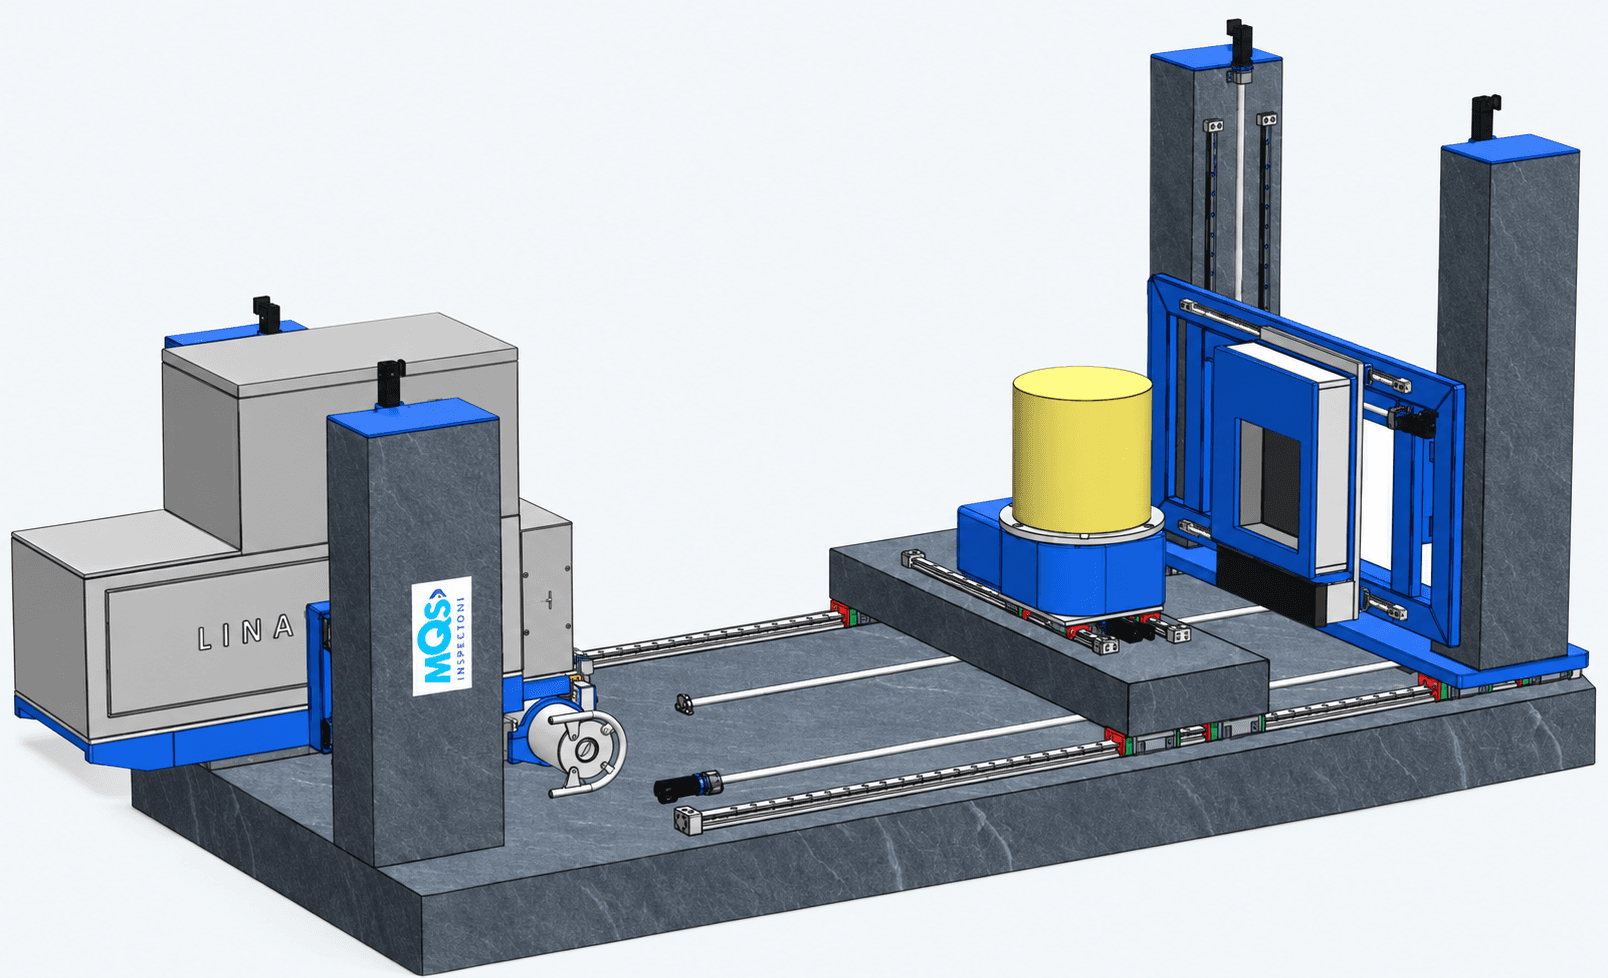
Accelerators combined with multi-axis manipulators for real-time NDT inspection, used for defect analysis in viscoelastic materials, metals and composites where volumes are large and geometries complex. The complete system is the accelerator, flat panel detector, manipulator and a control unit operated remotely from outside the inspection room.
- ManipulatorSeven axis for real-time inspection of solid propellants, plus a rotary table for small cylindrical objects
- Object envelopeCylindrical up to 500 mm diameter, 3500 mm length, 500 kg (customisable)
- Radiography quality1–2T or better for 50–250 mm steel (ASTM E-94)
- Defect analysisVoids, porosity with measurement, foreign-body identification
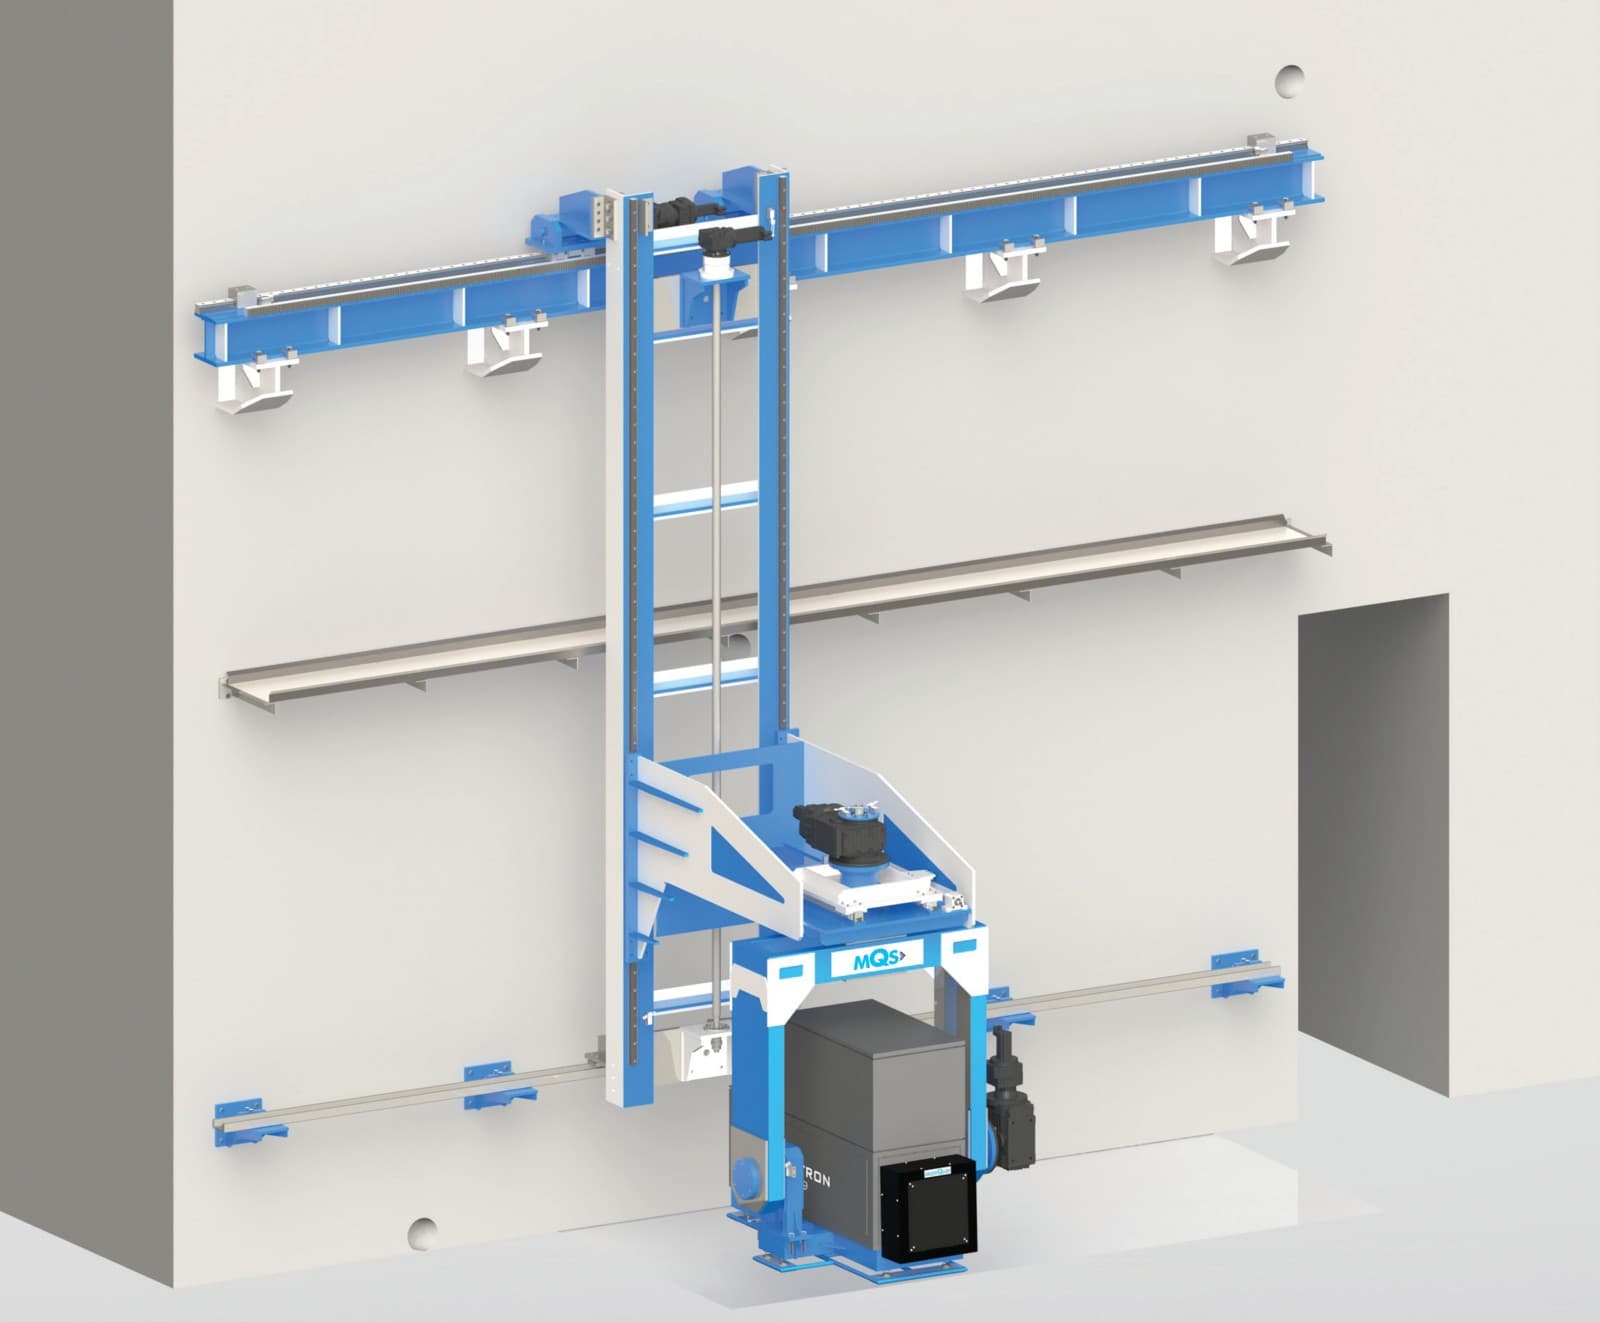
Wall Mount Manipulator Systems
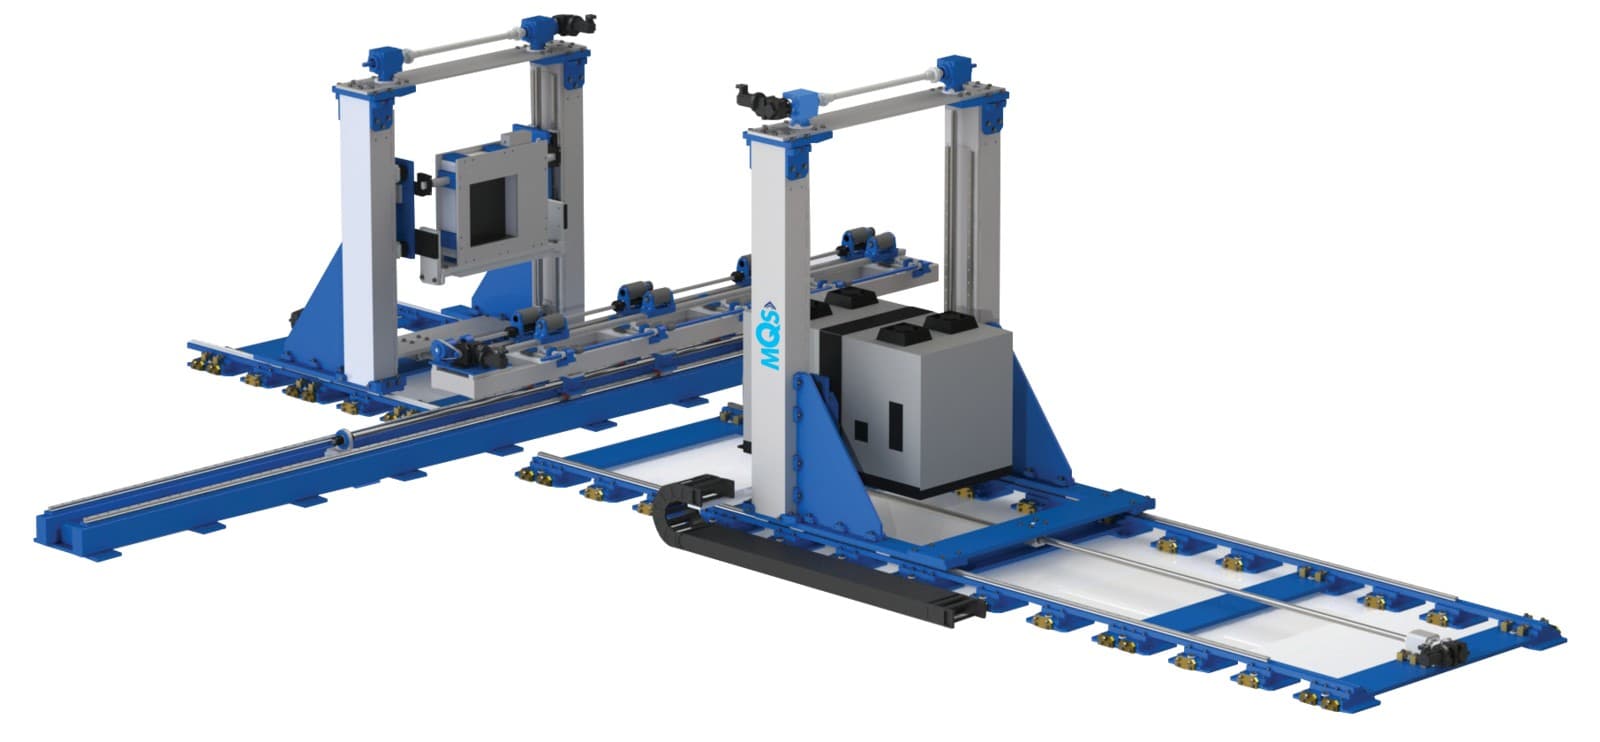
Where floor space is the constraint, a wall-mounted mainframe holds an X-ray head up to 15 MeV. Widely used in casting and foundry work, and compatible with both film and digital radiography systems.
- AxesLong travel, hoist, magnification, tilt and rotation
- Object size3 m height × 5 m diameter
- Tilt & rotation±60° at 0.1° stepper accuracy
MQHCT Series — High Energy Computed Tomography
High-energy CT for large, intricate parts — producing a measurable 3D volume rather than a projection, so porosity can be sized and located rather than estimated. Energy is chosen against the application, and the cell is configured around multi-axial manipulators, accelerators, detectors and imaging software.
- X-ray sourceDual energy Linatron, with optional dual-focus 450 kV industrial X-ray
- Imaging systemDigital flat panel detector to 16 MeV, with optional line detector
- HandlingCustom multi-axial manipulators for tube, flat panel and object
- Imaging softwareMQS Imaging Suite, VG Studio Max, Varex CBCT tools
- Control stationControl unit, operator workstation and image visualisation workstation
What Gets Inspected at These Energies.
Parts that are too thick, too dense, or too critical to be released on a sample check.
Rocket Motors & Propellants
Cracks, voids and debonds in grain and casing, at thicknesses no tube-based system can reach.
Castings & Pressure Parts
Porosity, shrinkage and inclusions in thick-section castings, valve bodies and pressure vessels.
Weldments & Components
Weld integrity in heavy fabricated structures where radiographic quality must meet ASTM E-94.
Technical Specifications
Digital Flat Panel Detector
| Parameter | Value |
|---|---|
| Operational energy range | 40 kV – 16 MeV |
| Active pixel area | 42.7 × 42.7 cm |
| Pixel pitch | 139 µm |
| Frame rate | 4 fps (1×1) · 15 fps (2×2) |
Beam Characteristics
| Parameter | Value |
|---|---|
| Focal spot size | Does not exceed 2.0 mm, measured by Full Width Half Max |
| Small focal spot | 1.0–1.5 mm on Mi-9 only, at reduced maximum dose rate |
| Field flatness | Measured at 1 m from target, ±7.5° off the central axis |
| Field symmetry | Beam asymmetry does not exceed 5% at 1 m from target |
| Shielding | Low leakage 1.0 × 10⁻³ (fraction) |
| Alignment laser | 533 nm Class II, 0.5 mW — not with the ULLP leakage option |
All Linatron models from Varex Imaging Corporation are designed and manufactured in accordance with EMC Directive 89/336/EEC and Low Voltage Directive 73/23/EEC.